Choosing between a cross-belt sorter and a tilt-tray sorter is one of the few decisions in a sortation project that is genuinely expensive to revisit. Both technologies discharge accurately at high rates, both are mature, and both will appear in a supplier’s proposal with similar headline throughput. The differences that matter are structural: how a parcel is carried, how many destinations fit in a given building, and what the machine asks of the maintenance team over ten years.
The selection therefore should not start from a throughput number. It starts from what you will actually put on the line and where it has to go, before the first quotation arrives.
How Each Technology Moves a Parcel
The mechanical difference is simple and the consequences are not. A cross-belt sorter carries each item on a short belt module mounted on a carrier; at the destination the belt runs sideways and sets the parcel down gently into the chute. A tilt-tray sorter carries each item in a tray that pivots and tips, so the parcel slides off under gravity.
From that difference follow most of the practical consequences:
- Discharge energy: a belt sets the item down; a tray tips it. Fragile and unstable items behave very differently on each.
- Item geometry: trays constrain the footprint that fits; belts tolerate longer and flatter items that overhang a carrier.
- Carrier count and spacing: each design has its own pitch, which sets how many items per hour a given loop speed can carry.
- Chute density: discharge geometry determines how tightly destinations can be packed along the line.
- Wear distribution: belts, motors and bearings on one; pivot mechanisms, trays and latches on the other.
Parcel Profile Is the First Filter
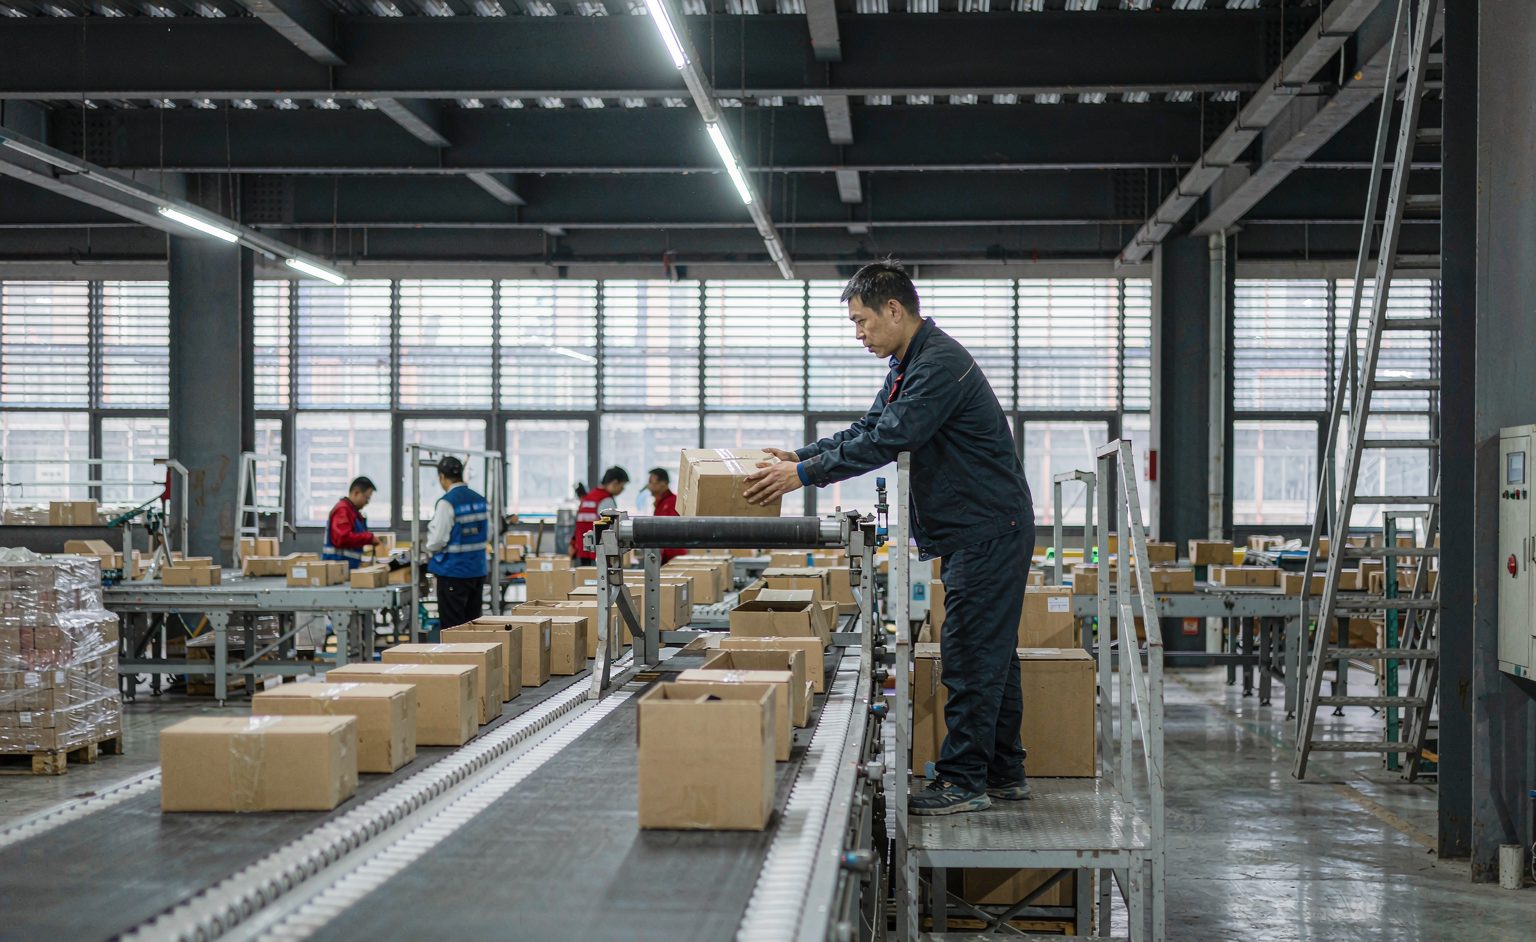
Before any discussion of speed, characterise the parcels: weight distribution, the share of soft or irregular packaging, the longest and flattest items, and the proportion that cannot tolerate a drop or a slide. Operations handling polybags, garments and flat cartons tend to find the belt discharge kinder to both the parcel and the downstream chute. Operations handling rigid, uniform cartons in a narrow weight band are less exposed to the difference, and the decision moves on to other criteria.
The second filter is the sort plan. Count the destinations you need today and the ones you expect to add, and be honest about the rate of change. Destination count drives chute count, chute count drives loop length, and loop length drives the building requirement – which is where the two technologies diverge most.
Footprint, Destinations and the Building
Chute density is usually the deciding constraint in retrofit projects. If a site needs a large destination count inside a fixed building, the question is not which technology sorts better but which one fits the destinations into the available length. That is a layout exercise, and it needs to be done with real chute widths, takeaway method and clearances – not with a rule of thumb about parcels per metre.
- Fixed building, many destinations: measure chute pitch against available loop length before anything else.
- Greenfield site: the building can follow the machine, so weight the operating and maintenance differences more heavily.
- Multi-level or mezzanine plans: structural loading and access for maintenance become selection inputs, not afterthoughts.
Maintenance Load and Lifetime Cost
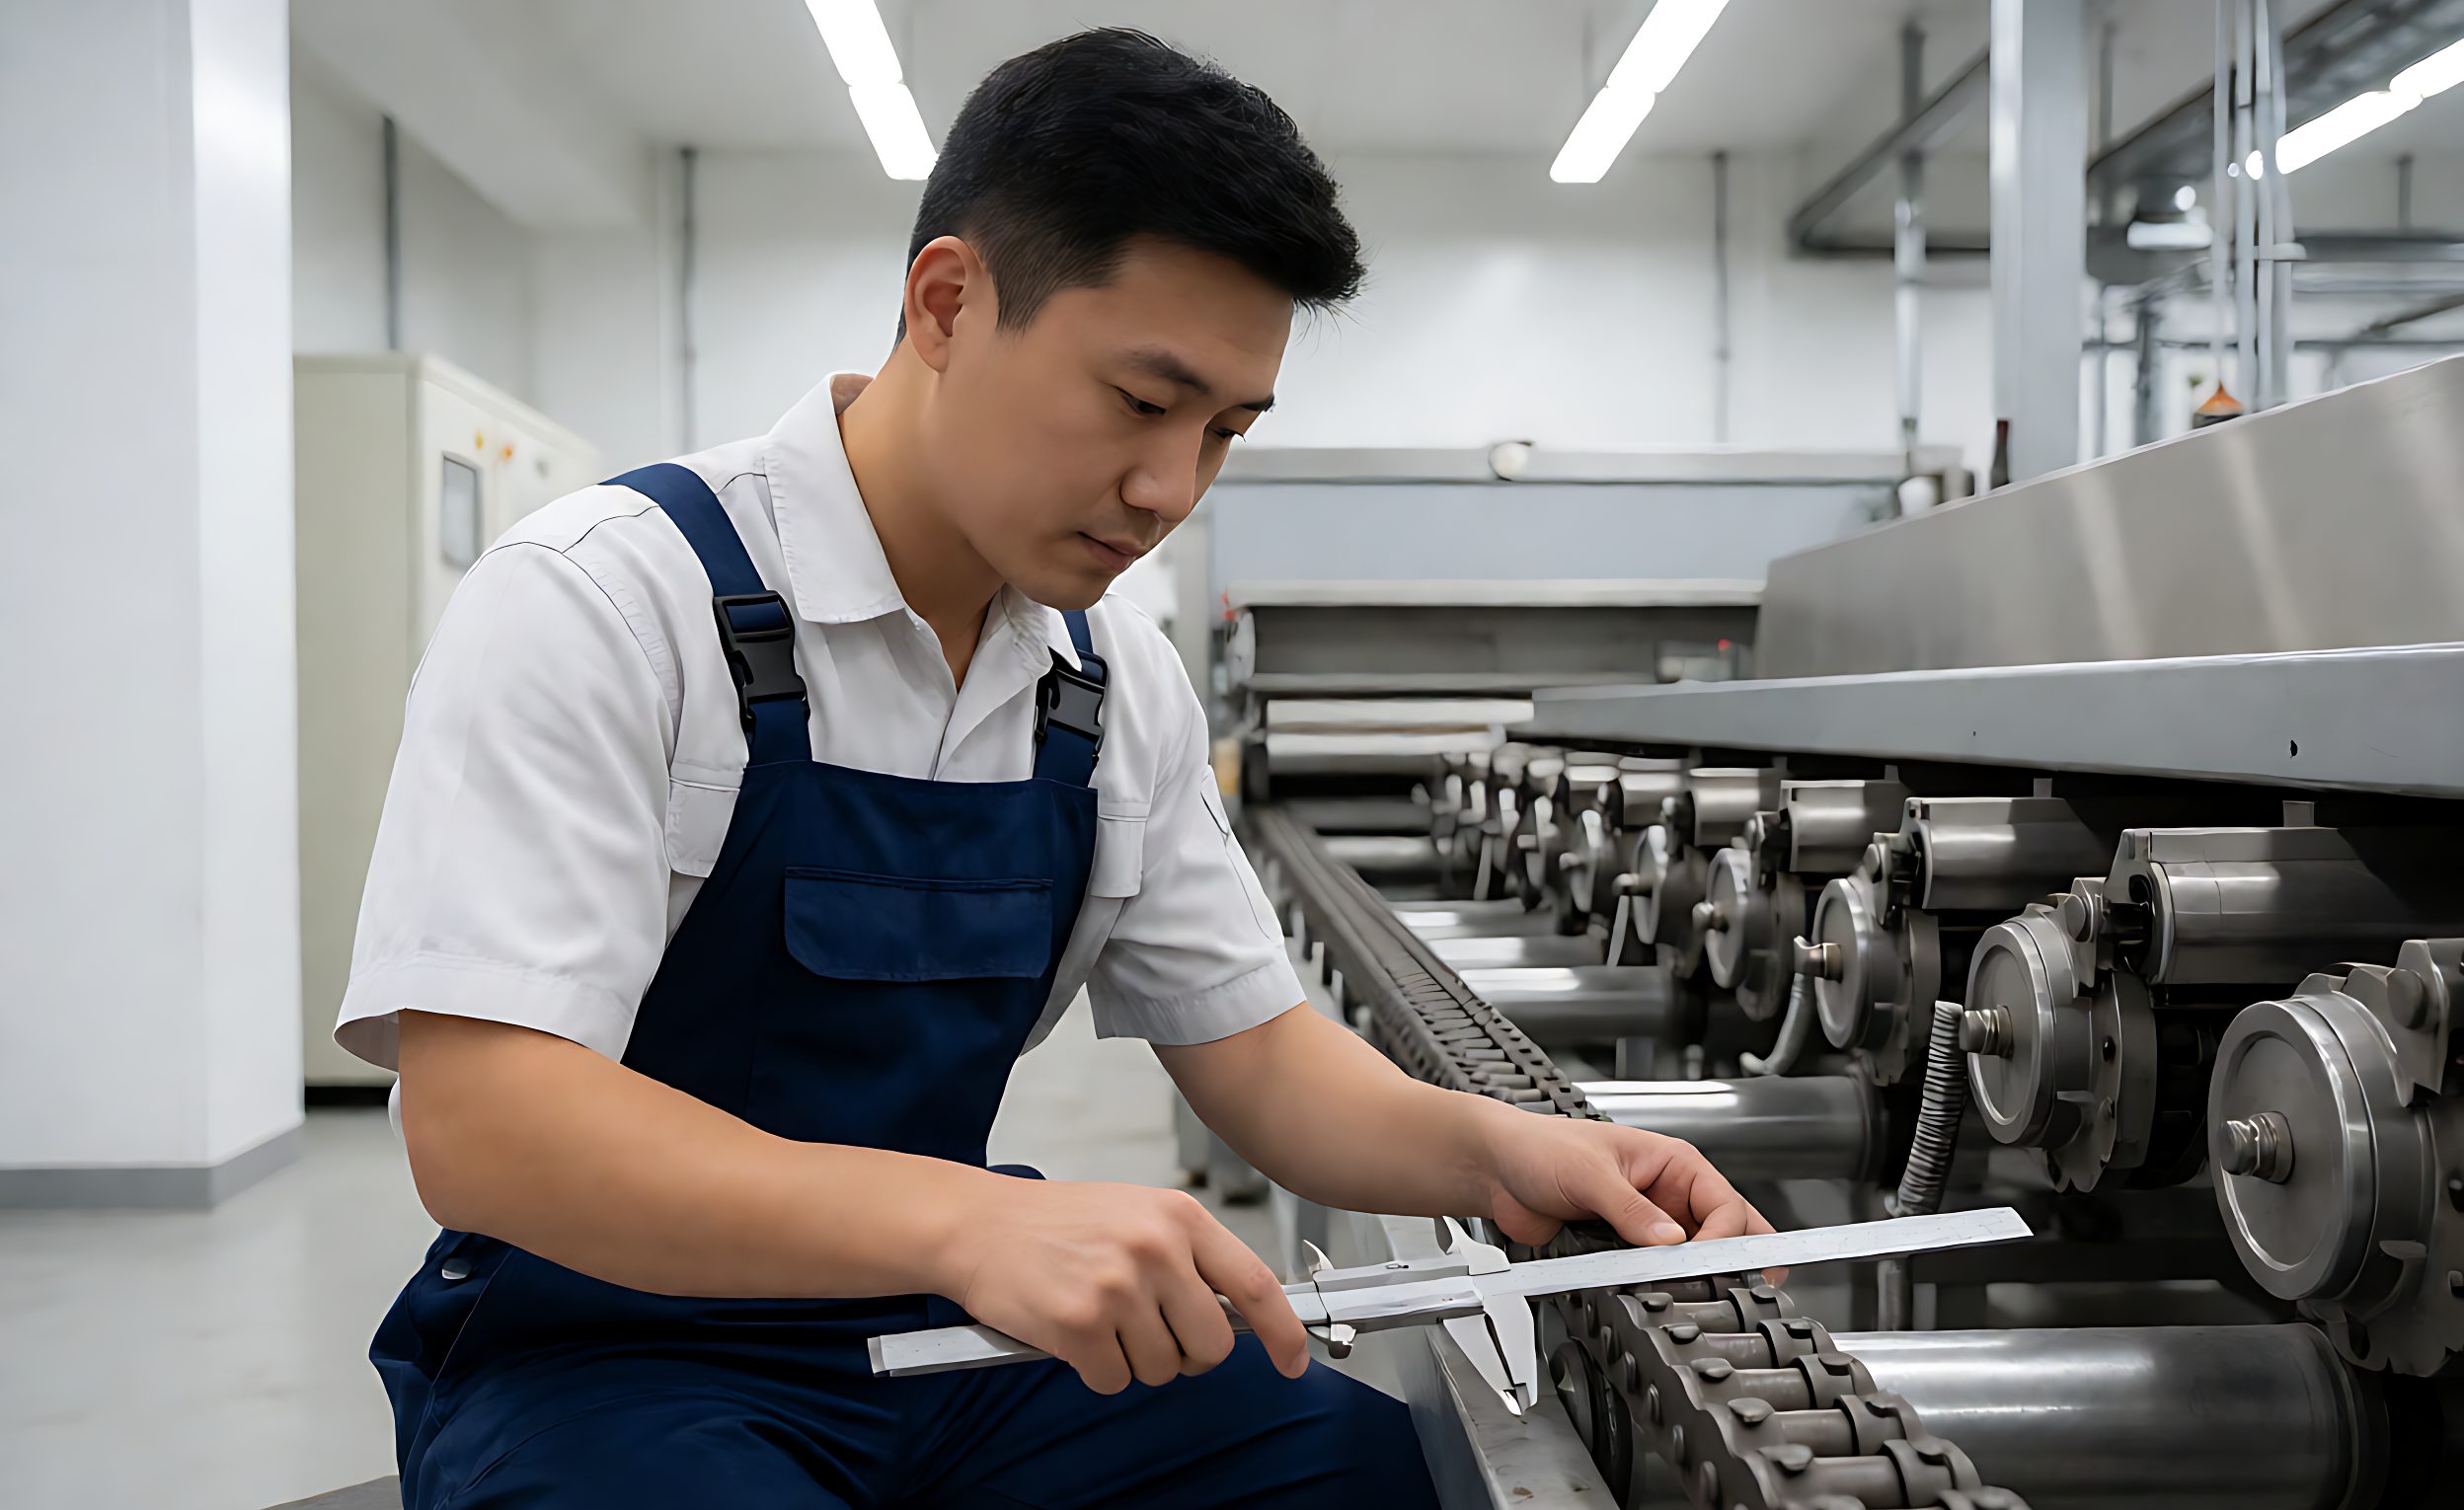
Both designs are maintainable; they are not maintainable in the same way. One concentrates wear in many small driven modules distributed around the loop, which favours planned replacement and condition monitoring but puts a large number of items in the spares list. The other concentrates wear in pivots, trays and latches, which favours mechanical inspection routines and typically involves heavier individual components when something does fail.
The honest comparison is the ten-year picture: replacement intervals, spares holding, labour hours and the cost of a bad failure. Build it before the decision rather than after it.
Technical Background
Both machines belong to the family of conveyor-based sortation systems in which each item is carried on a discrete carrier and discharged at a fixed destination. The buildings they serve are distribution centers, where the sort plan and the building geometry constrain each other. Because these are long-lived assets, the comparison belongs under total cost of ownership rather than purchase price – the acquisition cost is only the visible part of a ten-to-fifteen-year commitment.
Making the Decision Defensible
The most reliable way to choose is to give every serious supplier the same data package and compare their answers rather than their marketing. That package includes the parcel profile, the destination list with growth assumptions, the building constraints and the operating pattern. Where the proposals then disagree – on achievable rate, on chute count, on maintenance assumptions – the disagreement is the useful part of the exercise, and it should be resolved in writing before contract.
The wider selection context, including other technologies in the same family, is covered in the sortation system selection guide. Sizing the loop and chute bank against a budget is set out in the cross-belt buying guide, and the throughput claims in any proposal should be checked against how to verify CPH claims. The cost comparison that should decide between two viable options is built in the five-year total cost model, and the inputs suppliers need to quote accurately are listed in the RFQ data package.
Frequently Asked Questions
Which sorter handles fragile parcels better?
Generally the cross-belt, because the belt sets the item down rather than tipping it, though chute design and drop height influence the outcome at least as much as the carrier.
Which fits more destinations into a building?
It depends on chute pitch and loop length rather than on technology category. Measure the destination list against the available geometry before deciding.
Is one technology faster?
Both reach high rates. Achievable throughput is set by carrier pitch, loop speed and induction capability, so compare verified figures for your parcel mix, not nameplate numbers.
How do maintenance demands differ?
One distributes wear across many belt modules and motors; the other concentrates it in trays, pivots and latches. Both need planned routines, but the spares lists look different.
Can the two be mixed in one facility?
Yes, and it is common: a high-rate loop for the main flow and a second technology for a specific parcel class or returns process.
What data should I give suppliers for a comparison?
Parcel profile, destination list with growth assumptions, building constraints and operating pattern – the same package to every bidder.
Should the decision be revisited after installation?
Rarely. Physical layout and chute infrastructure make a change expensive, which is why the selection needs defensible inputs before contract.