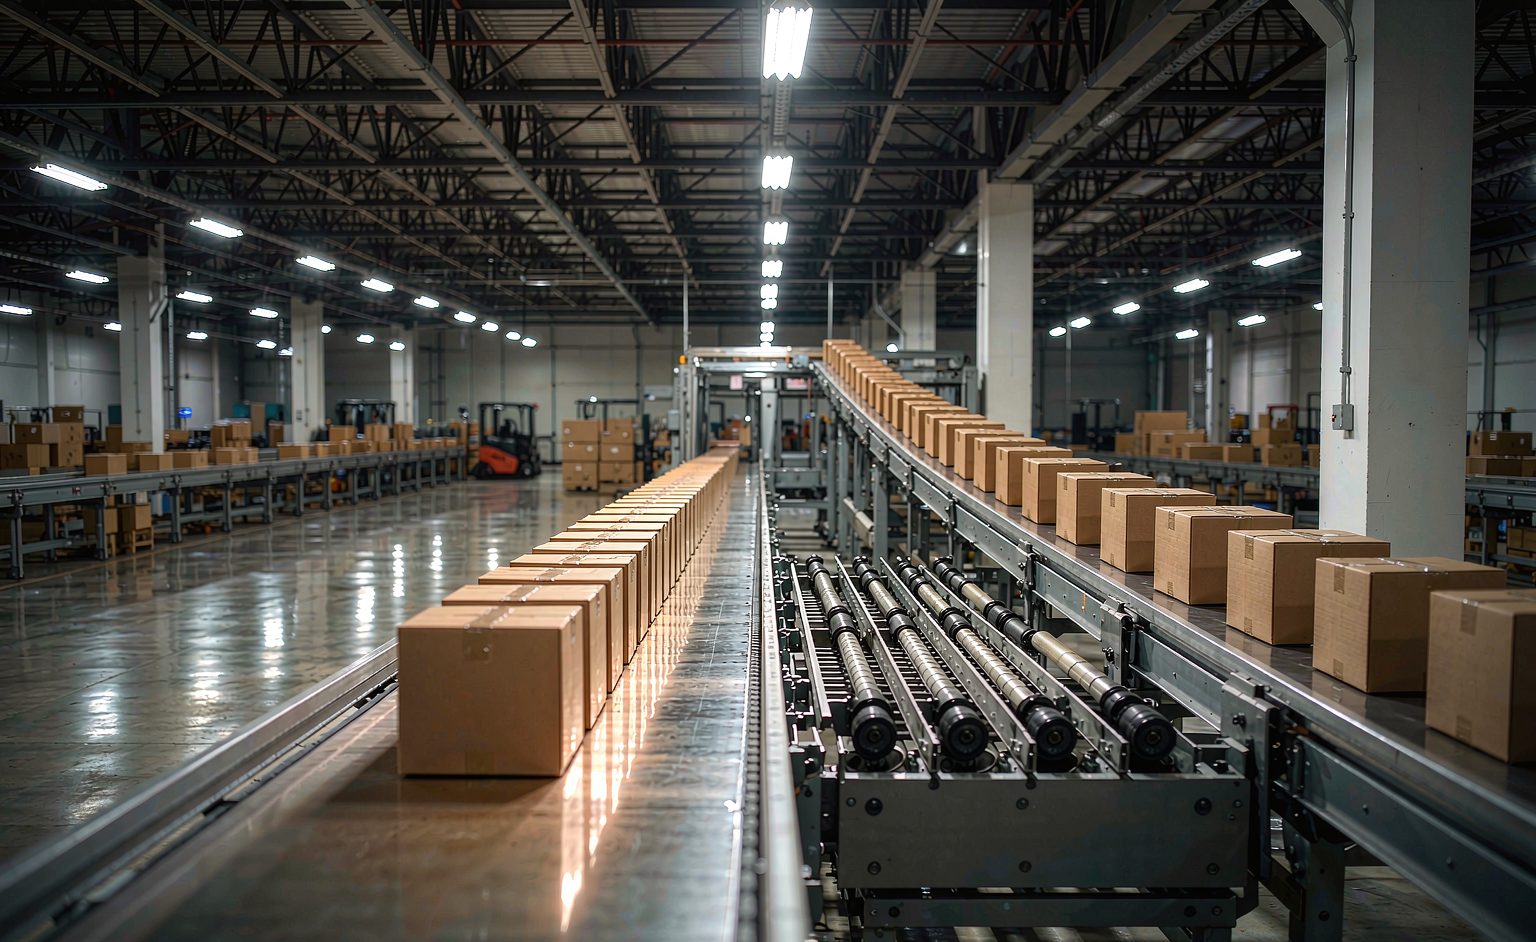
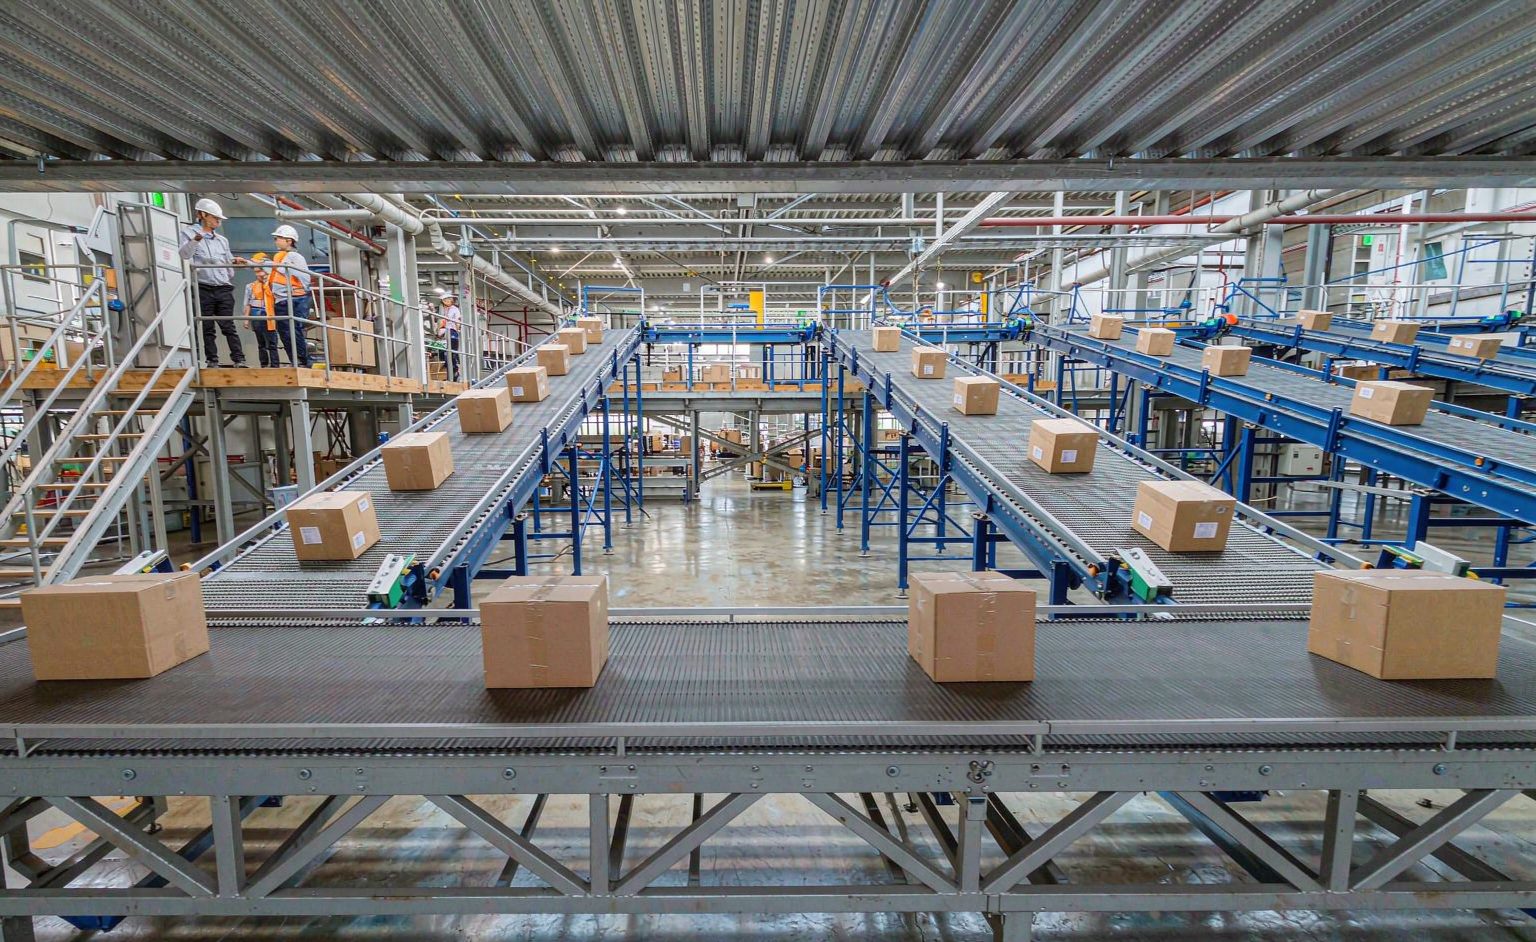
In high-volume logistics and e-commerce distribution, the ability to sort small to mid-sized packages rapidly, accurately, and without damage is a core competitive advantage. As manual labor costs rise and package shapes become increasingly irregular, traditional conveyor line diverters often fail to meet performance demands. This is where a cross belt sorter becomes essential.
A cross belt sorter system offers a highly reliable method for automated sorting. By placing each package on an individual, motorized belt conveyor cell that travels along a fixed track, these systems eliminate the physical sliding, tumbling, and friction associated with other divert mechanisms. This guide provides an in-depth technical overview of cross belt sortation technology, its performance capacity factors, primary applications, and essential B2B engineering selection tips.
Section 1: What is a Cross Belt Sorter? Mechanical Principles & Configurations
To understand why a parcel cross belt sorter is so effective, we must look at its underlying mechanical and control engineering. At its core, the system consists of a continuous chain of individually guided carriages (carriers) running on a steel tracking system. Each carrier is equipped with its own bi-directional mini-belt conveyor.
How the Sortation Cycle Works:
- Induction: Automated or manual induction lines feed parcels onto the moving carriers. The system calculatedly accelerates the induction conveyor belt to match the vector speed of the sorter, placing the package precisely in the center of the target carrier belt.
- Transport: The carrier transports the parcel along the track. Because the package sits completely stationary on the carrier’s belt, there is zero risk of shifting or damage during travel, even when navigating tight horizontal or vertical curves.
- Discharge: When the carrier aligns with its designated discharge chute, an onboard motor or localized mechanical actuator triggers. The carrier’s belt runs perpendicular to the main travel line, driving the parcel smoothly off the carriage and down the chute.
Loop (Horizontal) Sorters vs. Linear (Vertical) Sorters
Cross belt systems are configured in two primary layouts, depending on throughput requirements and warehouse floor space:
- Loop (Horizontal) Configuration: Carriers travel in a continuous, horizontal, closed-loop track. This layout allows for high-capacity setups because multiple induction zones can be placed along the loop, and sorting chutes can line both sides of the track. It is ideal for large-scale operations with hundreds of destination chutes.
- Linear (Vertical / Over-Under) Configuration: Carriers run in a straight, linear path, discharge packages to chutes on either side, and then return upside-down beneath the active sorting track. This “over-under” configuration is highly compact, utilizing a narrow footprint. It is incredibly cost-efficient for smaller warehouses, though it supports fewer total destination chutes.
Section 2: Engineering Parameters & Sorter Capacity Analysis
When designing a cross belt sorter for parcel sorting, engineers use mathematical models to calculate the theoretical and sustained throughput capacities. Sorter capacity is not a static number; it is a variable function of carrier pitch, linear speed, and system fill rate.
The Throughput Calculation Formula
To calculate the theoretical maximum capacity of a cross belt system, engineers use the following formula:
Where:
- S = Linear speed of the sorter track (meters per second)
- P = Carrier pitch (center-to-center distance between adjacent carriers, in meters)
- η = Induction fill rate (operational efficiency, typically between 75% and 90% depending on manual vs. automated induction)
- 3,600 = Number of seconds in an hour
For example, if a sorter runs at a linear speed of 2.0 m/s with a carrier pitch of 0.6 meters, and maintains an automated induction fill rate of 85%, the sustained operational throughput is:
Capacity = [ 2.0 / 0.6 ] × 3,600 × 0.85 = 10,200 PPH
Technical Parameter Comparison of TrueliSort Models
To help procurement managers match machinery with real operational requirements, the table below outlines the core technical specifications of two popular TrueliSort cross belt platforms.
| Technical Parameter | TrueliSort TR400-700 | TrueliSort TR500-1100 |
|---|---|---|
| Typical Application | Small parcel & mailer sorting | Medium to large parcel sorting |
| Carrier Size (W x L) | 400 mm × 700 mm | 500 mm × 1100 mm |
| Conveyor Line Link | TR400-700 Details | TR500-1100 Details |
| Rated Speed Range | 1.2 to 2.2 m/s | 1.5 to 2.5 m/s |
| Max Payload Capacity | Up to 15 kg | Up to 35 kg (configurable up to 50 kg) |
| Average Throughput Capacity | Up to 10,000 PPH | Up to 8,000 PPH (standard single-deck) |
| Compatible Package Profiles | Polybags, small cartons, envelopes | Large cartons, heavy mailers, odd-shapes |
Performance Note: Sorter speeds and payload capacities can be adjusted based on the physical properties of your items, such as the friction coefficient of the packaging material and the center of gravity of irregular loads. Actual system throughput is highly dependent on induction efficiency and layout parameters.
Section 3: Key Factors That Influence Cross Belt Sorter Capacity
While mathematical formulas provide a baseline, actual warehouse operational data will differ from theoretical data. To maintain high throughput, system planners must optimize multiple operational factors.
1. Induction Line Engineering
A cross belt sorter is only as fast as its induction feeding lines. There are three primary types of induction methods:
- Manual Induction: Human operators place parcels directly onto the sorter carriers. While highly flexible for irregular packages, human physical speed limits the induction rate to approximately 1,200 to 1,500 PPH per station. Multiple manual induction stations are required to fill high-speed loops.
- Semi-Automated Induction: Operators scan and place packages onto a smart queuing conveyor line, which automatically adjusts belt speeds to inject the item onto an empty carrier cell. This raises the rate to 2,000–2,500 PPH per station.
- Fully Automated Induction: Sorters are integrated with dynamic spacing conveyors and automated singulators that scan, measure, and inject parcels without human touch. Fully automated systems can operate at speeds that maximize the fill rate of high-speed carriers.
2. Recirculation Rates
If a parcel’s barcode is unreadable (a “no-read”) or if the designated discharge chute is full, the carrier cannot discharge the package. Instead, the parcel must travel around the entire loop again (recirculation). A high recirculation rate reduces the number of available empty carriers, effectively lowering the system’s net capacity. Integrating reliable scanning tunnels and maintaining active chute volume management are critical to minimizing recirculation.
3. Pitch Optimization and Multi-Carrier Carrying
For standard operations, each parcel occupies a single carrier. However, if your e-commerce facility handles a wide range of package lengths, you can utilize multi-carrier allocation. If a package is longer than a single carrier cell (e.g., a long poster tube), the system control software allocates two adjacent carriers to act as a single virtual cell, running both belts simultaneously to discharge the item. While this reduces the instant carrier availability, it allows the system to process a larger variety of SKU sizes without manual intervention.
Section 4: Primary Applications of Cross Belt Sortation
Because of their mechanical stability and versatile handling characteristics, cross belt sorters have become the gold standard across several high-volume logistics sectors.
1. E-commerce Warehouse Fulfillment
An e-commerce center processes thousands of multi-item orders daily. A cross belt sorter for ecommerce warehouse operations is highly valued because it handles a diverse array of non-rigid, soft packaging. Thin plastic mailers, lightweight bubble envelopes, cosmetics, and soft apparel can easily jam sliding shoe or pop-up wheel sorters. The active belt-to-belt transfer of a cross belt system ensures these soft items are handled cleanly without catching or jamming.
2. Express Parcel & Postal Sorting Hubs
Courier, express parcel, and postal hubs require high-capacity, multi-destination routing systems. These facilities often operate in severe, time-sensitive windows (e.g., overnight sorting). Implementing a rugged express parcel sorting solution featuring heavy-duty cross belt loops allows postal hubs to route tens of thousands of shipments directly to dispatch vehicles or regional logistics line-hauls with high accuracy.
3. Third-Party Logistics (3PL) Operations
3PL operators manage logistics for multiple business clients under one roof, meaning their SKU profiles can change completely from month to month. The extreme flexibility of a cross belt system allows 3PLs to onboard new clients with completely different package dimensions or fragile characteristics without needing to overhaul their physical sorting machinery.
Section 5: Selection Tips: How to Choose the Right Cross Belt Sorter System
For a procurement or operations manager, selecting the correct cross belt system requires evaluating both present operational volumes and future growth plans. Consider the following engineering selection guidelines:
1. Match Your Parcel Dimensions to Carrier Sizes
The maximum length of your standard parcel profile dictates your minimum carrier length. If 95% of your packages are under 600mm, a carrier length of 700mm—such as the TR400-700—is ideal, as it keeps the carrier pitch short, maximizing your potential PPH. However, if you routinely handle larger shipping cartons up to 1,000mm, selecting a larger platform like the TR500-1100 is necessary to prevent packages from hanging over carrier edges.
2. Evaluate Floor Space vs. Destination Chutes
If you need to sort to a high number of destinations (e.g., 100+ postal routes), a horizontal loop system is required, as it can curve around columns and make full use of the building’s length and width. If you only need to sort to 10–30 dispatch zones and are working with limited warehouse width, a linear (vertical) “over-under” system will save valuable floor space while still delivering high performance.
3. Ensure High-Speed Scan Tunnel Compatibility
A sorting system is only as fast as its data handshake. Your sorter must be matched with an advanced scan tunnel capable of reading barcodes on the top, sides, front, and back of packages in real-time. Ensure your system provider integrates high-resolution CCD cameras and dimensioning sensors that communicate instantly with the sorter’s PLC.
Section 6: Supplier Evaluation and Project Implementation
Selecting a high-quality cross belt sorter system is not just about comparing equipment prices; it is about finding a long-term engineering partner. Automated sortation projects represent custom integration systems that must align with your physical facility and digital architecture.
1. Custom Engineering & Factory-Direct Support
Avoid rigid, pre-designed sorting packages. Working with a factory-direct manufacturer like TrueliSort ensures that your system layout is custom-designed for real operations. This custom approach includes tailoring chute angles, designing optimal induction paths, and adjusting track heights to clear existing racking or mezzanine support structures.
2. Rigorous Pre-Shipment Testing (FAT)
To minimize installation delays, ensure your supplier performs a complete Factory Acceptance Test (FAT). The manufacturer should set up a physical portion of your sorter loop, run it at rated operational speeds, and test it with your specific package types to verify tracking precision, motor calibration, and noise levels prior to shipping.
3. Post-Installation Commissioning and Maintenance
The complexity of high-speed sortation requires professional on-site commissioning, integration testing with your Warehouse Management System (WMS), and hands-on maintenance training for your local operations team. Make sure your supplier provides comprehensive technical documentation, a robust spare parts package, and remote diagnostic support options to address any operational queries during peak seasons.
Capacity figures are only comparable once the belt architecture is fixed. A cross belt and a narrow belt sorter of similar footprint diverge sharply in sortation points, parcel profile tolerance, and sustainable throughput, so validate the configuration before committing to a capacity target: compare cross belt and narrow belt sorter capacity and applications.
Frequently Asked Questions
Q1: What is the difference between a loop (horizontal) and a linear (vertical) cross belt sorter?
A loop (horizontal) cross belt sorter runs in a continuous horizontal plane. It can support hundreds of destination chutes on both sides of the track and accommodate multiple induction zones, making it suitable for complex, high-throughput hubs. A linear (vertical or over-under) cross belt sorter runs in a straight line, returning carriers underneath the active sorting path. It occupies a much narrower footprint and is more cost-effective, but supports fewer destination chutes and lower overall capacity.
Q2: How does parcel slip affect the sorting accuracy of a cross belt sorter system?
Parcel slip occurs when the friction between the carrier belt and the package is insufficient during acceleration or deceleration. To mitigate slip, modern cross belt sorters use high-friction, anti-static belt materials and execute controlled speed ramping via localized motor drivers. Precise tracking is maintained using rotary encoders and photo-eye sensor arrays, allowing the PLC to adjust the discharge timing dynamically based on calculated slip tolerances.
Q3: What are the typical maintenance requirements for a cross belt sortation system?
Routine maintenance includes monthly inspections of carrier belt tension, checking the wear on polyurethane track wheels, cleaning optical sensors at induction and divert points, and ensuring reliable data transmission through the wireless communication or infrared control system. LSM (Linear Synchronous Motor) or friction-drive systems should be checked for gap clearances and magnetic alignment quarterly.
Q4: Can a cross belt sorter handle irregular packages like tubes or round containers?
Yes. Because a cross belt sorter carries the parcel on an individual, self-contained conveyor cell, it does not rely on the item having a flat bottom or sliding surface. Cylindrical tubes, flexible polybags, and round containers remain stationary relative to the carrier belt during transport, preventing the rolling or tumbling associated with roller or wheel diverters. At the discharge point, the active driving motion of the belt ensures a clean, controlled release.
Compare Sorting Equipment for Your Operation
Are you looking to install a new high-speed cross belt sorter or expand an existing logistics sorting facility? The TrueliSort engineering department can help you design an optimal layout, select the right carrier capacities, and calculate accurate system throughput estimates.
We provide factory-direct customized parcel sorting systems engineered for real-world operations, including full installation, FAT testing, and local commissioning support.
Contact our engineering team to plan your parcel sorting project or email us at business@truelisort.com to schedule a technical consultation.